Send Your RFQ to Synbase Steel
Prefer to send drawings, BOMs or attachment lists by email? sales@synbasesteel.com
Updated October 2026
Product: longitudinal submerged arc welded pipe. Comparison Unit: a specified pipe lot from a named producing mill. Start with the engineer-approved spec, quantity, coating and delivery point. Compare prices only after these fields are matched.
A mill that suits a long pipeline run may be an awkward choice for six replacement lengths. In the pipe industry, the lowest price may become the highest after taking coating and freight into account. This guide focuses on shortlisting suppliers, showing exceptions and illustrating how to compare offers. For Synbase’s product range and an inquiry, see our LSAW pipe supply options.
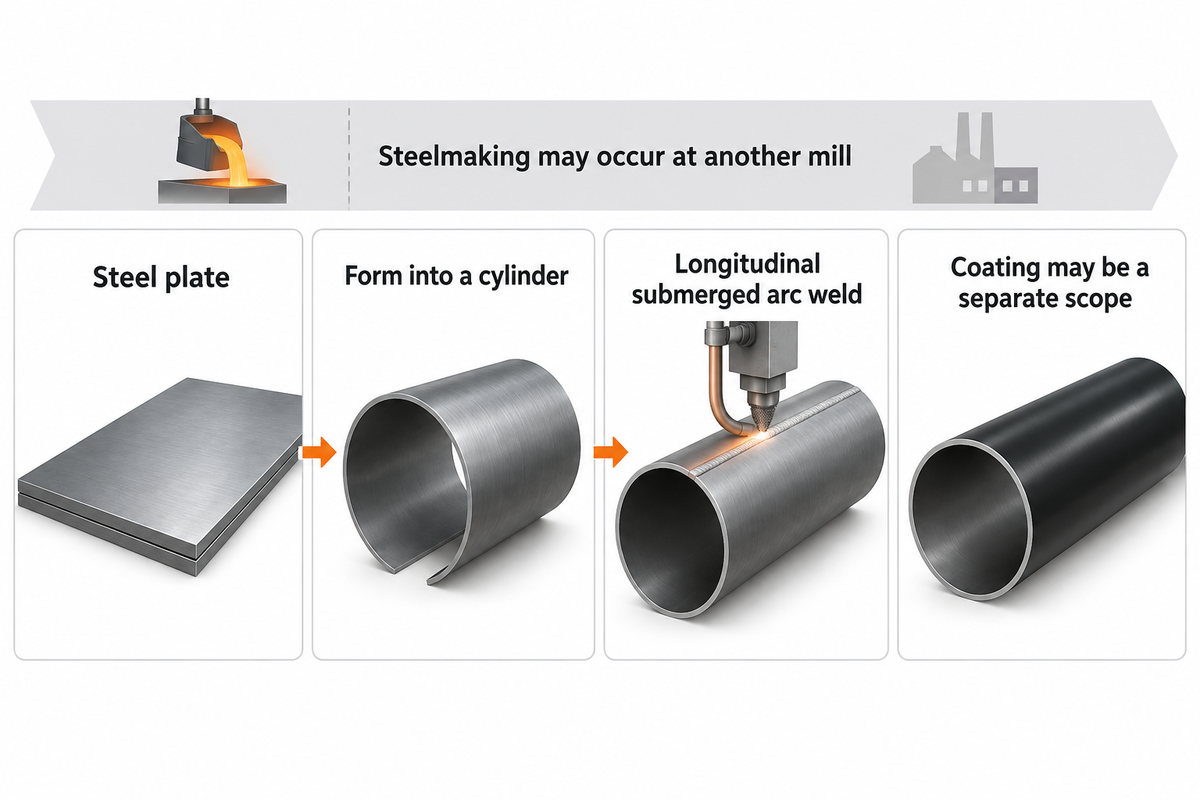
An LSAW pipe manufacturer forms steel plate into a cylinder and joins its longitudinal edges using submerged arc welding. Pipe production may include expansion, testing and coating at the producing mill, while steelmaking or plate supply may occur at another mill. Compare the named producing mill and contracted work when two sellers offer the same pipe type.
Longitudinal submerged arc welded pipe is also known as SAWL. The longitudinal weld seam runs parallel to the pipe as opposed to wrapping around it in a spiral. Inner and outer welding can be combined in a single production process. Submerged arc welding technology uses a covering flux over the arc. The LSAW steel pipe manufacturing process guide provides information on various terminology and the forming stages.
A steel producer may make the plate. Pipe factories may form it and weld it, and a separate entity may coat or sell the finished lengths. An integrated carbon steel pipe manufacturer may perform any or all of these functions. If a change of seller means an undisclosed change of mill, then that’s misleading. A generic steel tube listing is too broad to capture this. Identify the longitudinally submerged arc welded product and its ordered specification.
Line pipe for long-distance oil and gas pipelines requires an order specification to state the service conditions, as well as the dimensions. Engineering sets the requirements. Procurement then determines the production route and supplier that meet them. Weld quality belongs in the inspection scope, along with required methods and acceptance criteria carried in the purchase order.
JFE Steel’s Fukuyama mill and Dura-Bond’s Steelton facility are good examples of documented production routes for comparison. JFE explains UOE and NEO Press forming; Dura-Bond explains straight seam DSAW with U/O forming and hydraulic expansion. Use their plant specific information to create a short list, and match the order to the offered facility.
| Producer example | Officially described operation | Useful buying comparison |
|---|---|---|
| JFE Steel, Fukuyama, Japan | SAWL using UOE and NEO Press forming | Compare the forming route with the required length and coating range. |
| Dura-Bond, Steelton, Pennsylvania | Straight-seam DSAW; stated diameter 24–42 in, grades up to X80 and lengths up to 80 ft | Compare a U.S. producing location with the destination and the specified lot. |
These are some examples from the producers’ published product info, reviewed in Oct 2026. When evaluating straight seam welded pipe, consider the combined requirements of the pipe diameter and length. A sales office in either Texas or California can mean pipe is made elsewhere, so use shipment origin and delivery point when evaluating logistics.
Synbase’s company profile provides background for its supply role. Discuss its role as a supplier separately from the item-by-item acceptance of each pipe lot. A supplier combining pipe with other steel products could consolidate a project, but the specific LSAW order requires a named production source. For an order shipped from China, the production of LSAW and export handover should appear as separate entries on the schedule.
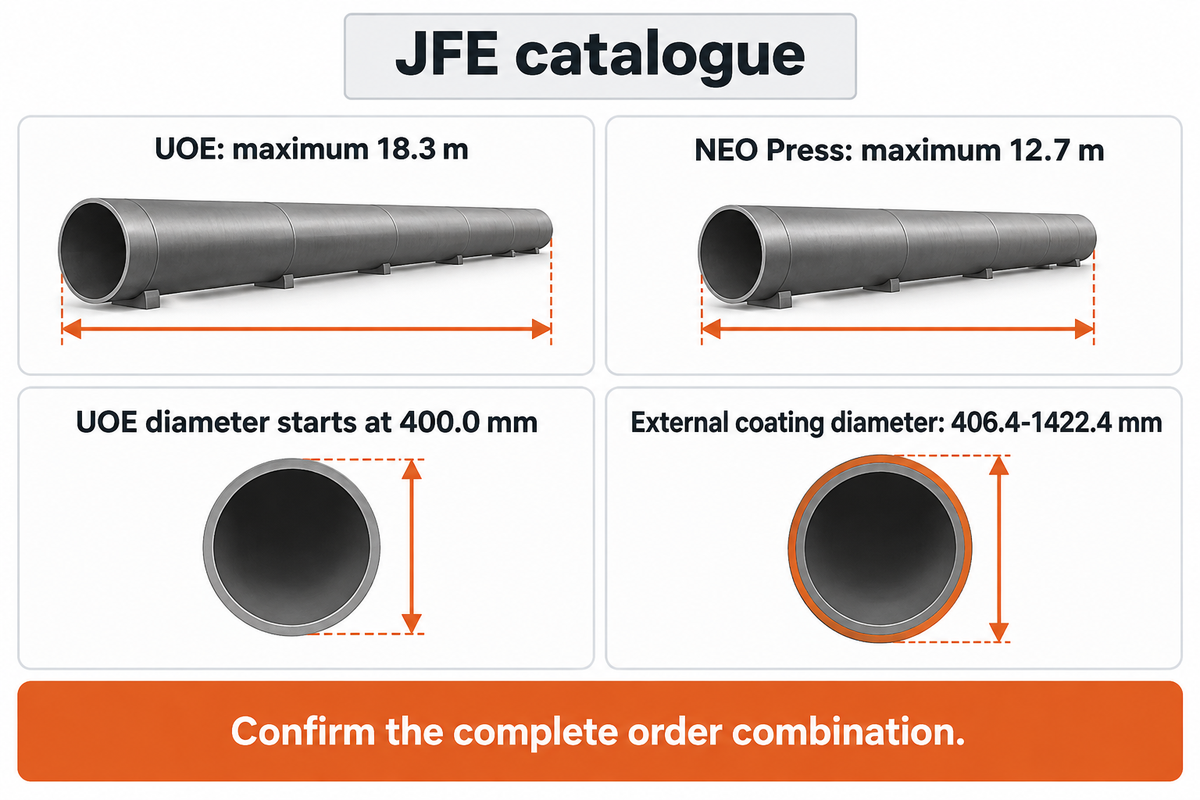
JFE’s SAWL catalog lists maximum lengths of 18.3 m for UOE pipe and 12.7 m for NEO Press pipe. This makes length a practical factor to consider. Consider diameter, wall thickness, grade, length and finish as one order combination and separate any line item that falls outside this offered combination.
UOE and JCOE describe the forming process of steel plate before longitudinal seam welding and expansion. Neither process name alone selects the more appropriate manufacturer for a project. Steel manufacturing establishes the properties of the plates; forming equipment, welding processes and inspection then contribute to the finished pipe. Comparing quality LSAW steel pipes therefore involves comparing the required tests and the forming route.
The same JFE catalogue puts its external coating range at 406.4-1422.4 mm outside diameter and 9.0-18.3 m length. Its UOE pipe range starts at 400.0 mm. A 400 mm pipe inquiry therefore requires a separate coating solution, rather than assuming that all forming sizes travel through the coating line which is listed. This is a catalogue-based comparison, and order availability is established in the quotation.
The 4-Fit Mill Selector compares the technical lot, quantity, finishing and handover before the buyer compares price.
Use the following worksheet for every line item. Engineering specifies; procurement allocates the supply; finance compares costs only after the exceptions are visible.
| Fit check | Order entry | Decision if it differs |
|---|---|---|
| Technical: outside diameter | Diameter in mm or in, with tolerance | Keep the approved size; route the exception to engineering. |
| Technical: wall and grade | Wall thickness in mm and specified grade | Evaluate the pair, not two independent catalogue maxima. |
| Technical: service | Engineer-approved pressure, temperature and toughness requirements | Reject an offer that omits required service qualification. |
| Technical: length | Length in m and permitted length variation | Split the lot or revise the route with engineering approval. |
| Quantity: ordered amount | Pieces, metres and agreed mass basis | Compare stock allocation with a new production lot. |
| Quantity: delivery splits | Quantity required at each delivery date | Price storage and partial shipments separately. |
| Finishing: coating | System, dimensions, cutbacks and acceptance requirements | Assign a compatible coating line and its completion date. |
| Finishing: release | Required tests, inspection points and records | Resolve missing work before treating the lot as ready. |
| Handover | Named destination, transport scope and agreed rule | Recalculate the offer at the same delivery point. |
Example: an order contains 12 m and 18 m lengths. A proposed route capped at 12.7 m can cover the first length but not the second. Split the 18 m lot to a compatible route, or have engineering assess a revised length arrangement. Requiring one seller can still work if that seller manages two disclosed production allocations.
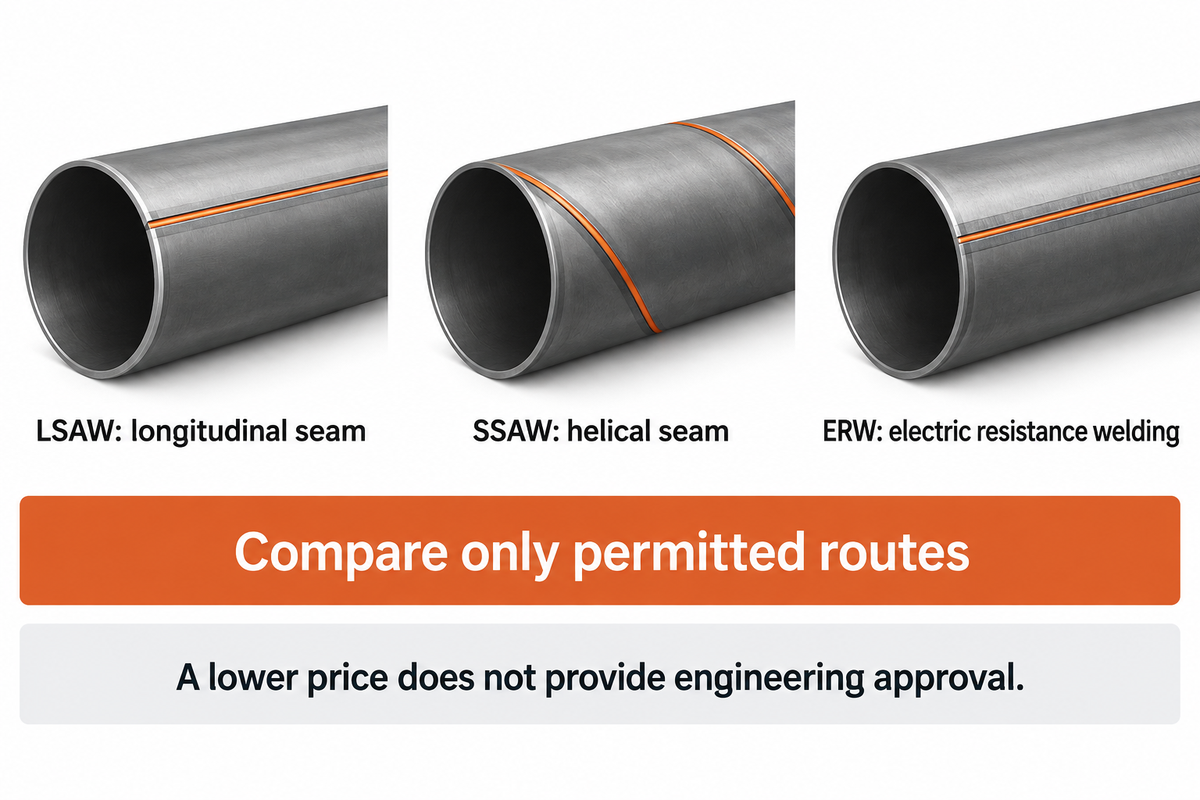
An approved alternative can widen the supply options for a welded steel pipe order. LSAW uses a longitudinal seam, SSAW uses a helical seam and ERW uses electric resistance welding. Start with the manufacturing methods allowed by the project specification, and then compare available sizes, testing, finishing and delivery of permitted routes.
Spiral submerged arc welded pipe can be permissible with longitudinal products in a pipeline specification. An offer for SSAW pipe still needs to comply with the allowed manufacturing route. Mechanical properties, dimensional requirements, inspection and the design requirements remain part of the selection.
For example, an inquiry for oil and gas transportation can permit either longitudinal or spiral welded pipe, while another permits only LSAW pipe. For the former, two technical offers can be invited for the same required scope. The latter requires engineering approval before a different pipe type can be invited for a commercial comparison. A lower price won’t provide that approval.
Our welded steel pipe comparison includes other routes. The ERW pipe options page is useful when electric resistance welded pipe is permissible. Seamless and welded steel pipes have different manufacturing routes; switching to seamless pipe also requires a specification match.
A new mill order fits a specified production lot; stock is useful when appropriate existing lengths and records satisfy the requirement; a project supplier can combine several sources and steps of work. Choose the model by the work the order demands. Quantity helps, but project-specific inspection and material records can rule out an otherwise convenient stock offer.
The Canada Energy Regulator’s pipeline materials quality assurance paper describes the difference: millrun orders allow for additional project requirements, and stock kept by manufacturers or distributors may have been manufactured to the industry’s minimum requirement. Buying from a manufacturer’s own stock requires a match to the project’s inspection requirement.
| Buying situation | Starting route | What must travel with it |
|---|---|---|
| Six urgent replacement lengths | Suitable stock | Matching dimensions, grade and required records |
| Repeated lots of one approved specification | Mill production agreement | Lot quantities and scheduled releases |
| Pipes with different diameters | Split mill allocation | Producing source for each size |
| Special project inspection | Qualified new production or fully matching stock | Required hold points and test records |
| Coated pipe from an uncoated stock lot | Stock plus assigned coater | Coating specification and completion date |
| Several approved pipe materials | Project consolidation | Separate material identities and documents |
| Demand for LSAW split across site arrivals | Scheduled supply | Storage, handling and shipment responsibilities |
| Long-length large-diameter steel pipe | Compatible mill and transport plan | Length-specific handling and receiving arrangements |
| One seller coordinating several factories | Project supplier | Named production sources and one agreed exception process |
When replacing six pipe lengths, for example, look for stock first. If test records for that stock omit a mandatory requirement that can’t be satisfied after manufacture, seek out a compliant production lot. For the work required, there’s no useful universal minimum order: the available material and the work required decide it. The description “high-quality steel pipes” in the pipe industry needs to be checked against the grade, tests and acceptance requirements of the buyer.
Comparable steel pipe quotations cite the same technical lot, quantity, finishing, inspection and delivery points. Separate fixed order charges from charges per tonne when comparing total costs for each quote. Add the same cost categories to each quote to compare total costs on the same basis. Add import, receiving and transport costs to the pipe cost when calculating the landed cost. Separate transport risk from who pays freight costs.
A steel pipe market price quoted without a grade, quantity, and delivery basis isn’t a usable project budget. Send the same purchase schedule to each bidder and compare the returned scope, line by line.
The U.S. International Trade Administration’s landed cost guidance includes the goods, insurance, freight, tariffs, taxes, and other charges. This is broader than a pipe and freight subtotal. Identity of the origin and destination as well as the producer/exporter should be included in the import cost assessment. An import cost assessment should be done by an import cost specialist.
The Same-Scope Quote Test compares bids for the identical pipe lot with the same work included.
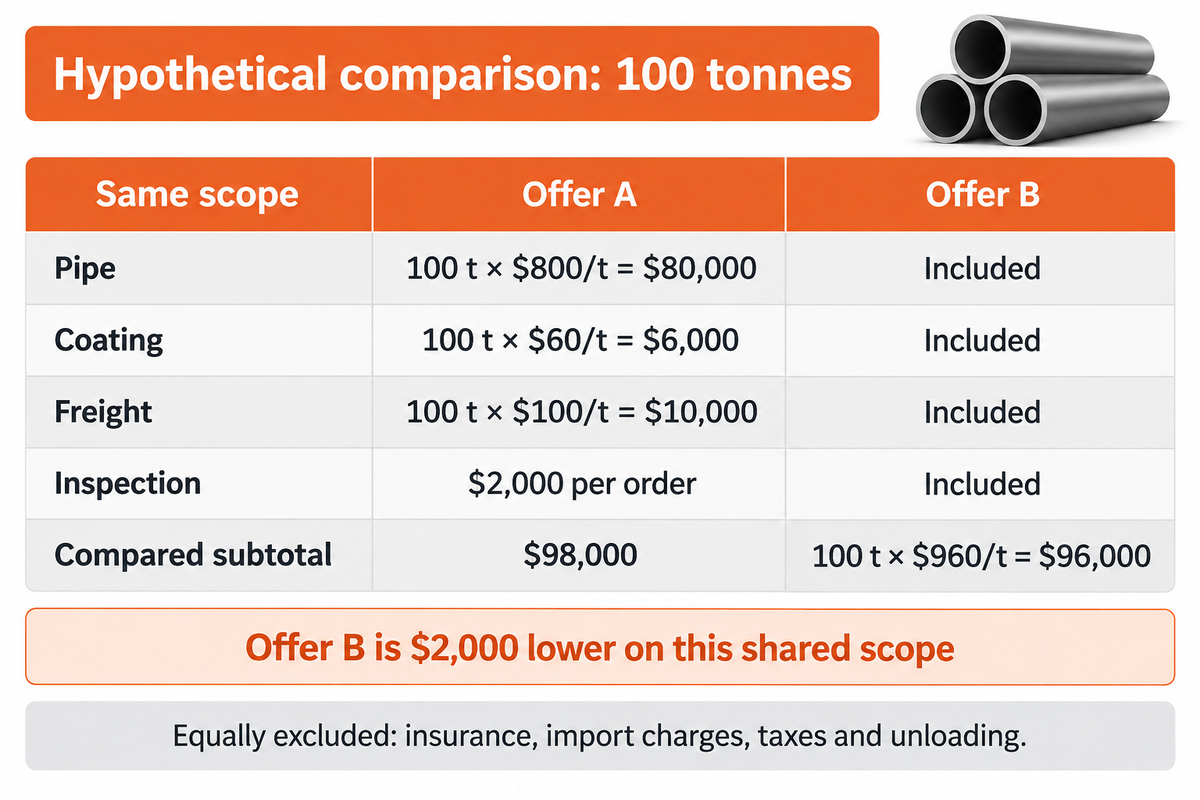
Assumed inputs: 100 tonnes of identical approved pipe, the same coating and inspection work, and freight to the same named destination. Offer A lists pipe at $800/t, coating at $60/t, freight at $100/t and inspection at $2,000 per order. Offer B includes those four items at $960/t. Insurance, import charges, taxes and unloading are excluded equally. These are teaching figures, not current market quotations.
| Same scope | Offer A | Offer B |
|---|---|---|
| Pipe | 100 t × $800/t = $80,000 | Included |
| Coating | 100 t × $60/t = $6,000 | Included |
| Freight | 100 t × $100/t = $10,000 | Included |
| Inspection | $2,000 per order | Included |
| Compared subtotal | $98,000 | 100 t × $960/t = $96,000 |
Offer B is $2,000 lower on this shared scope. The result changes if its included coating, inspection or freight differs. Procurement resolves those exceptions before finance adds the remaining landed costs. For quantity checks, the pipe weight calculator helps estimate mass; the quotation must still state whether invoicing uses theoretical or actual weight.
“This means that the risk does not transfer upon arrival of the goods at the named place or port of destination.”
If Incoterms® C are applicable, the seller pays transport costs to the named destination while risk transfers earlier. If Incoterms® D are applicable, risk transfers at the named destination under the agreed rule. State the agreed Incoterms® rule and version, the named place and price to ensure two freight-inclusive offers don’t mask different handovers.
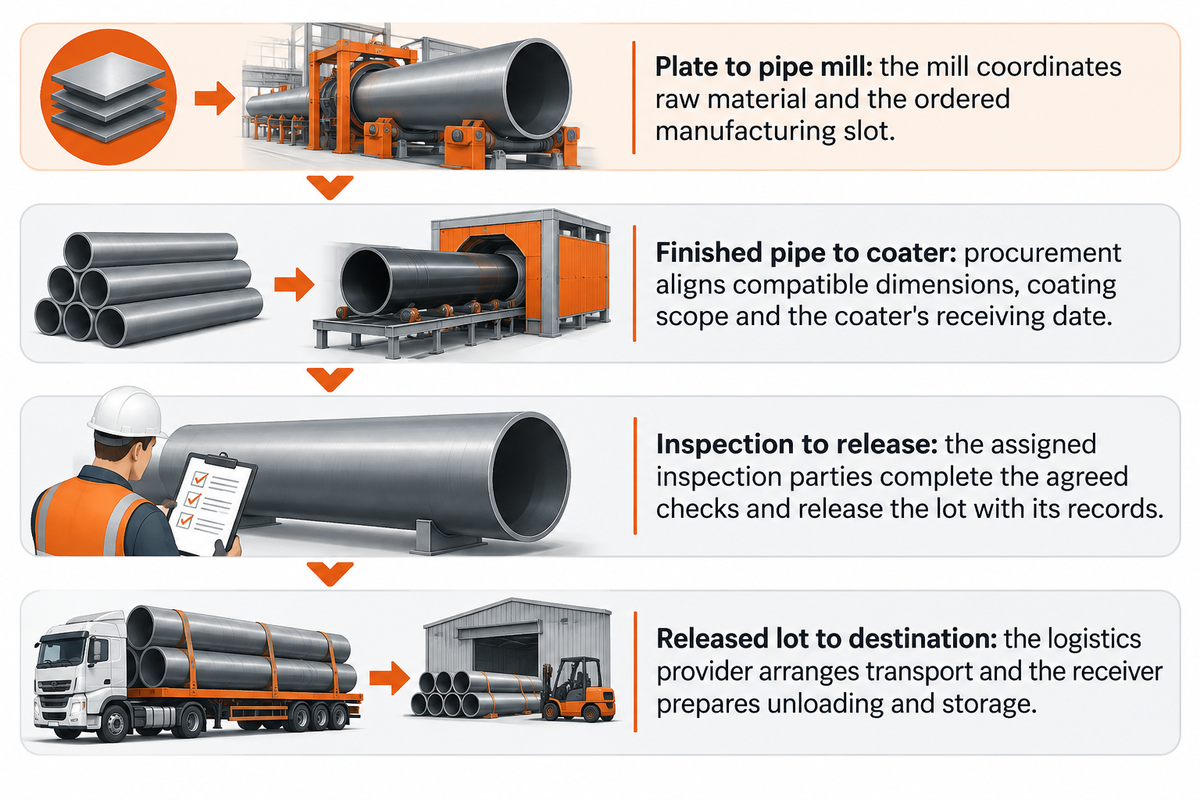
There are a number of handoffs between the pipe lot and finishing and transport. Each handoff needs an owner and date. Pipe ready at the mill can still be waiting on coating work or a release document. Also, pipe of a certain length can be awkward to transport. Think about pipe logistics along the production process.
Coating provides corrosion resistance via a specified system and its application requirements. JFE’s catalog separates external systems, such as fusion-bonded epoxy and three-layer polyethylene, from internal epoxy coatings. Maintain coating dimensions and acceptance work in the same inquiry as steel pipes; adding them later, after the mill allocation, can change the required production arrangement.
Handling must be addressed in the order. PHMSA’s material and weld failure fact sheet describes transit fatigue associated with improperly supported pipe. It’s considered a historical reason to specify handling arrangements, not a current failure rate for LSAW manufacturers.
If API licensing is part of the purchasing requirement, use the API Composite List Directory to check the named facility and relevant specification. The entry is for the named facility and a group logo doesn’t identify the producing mill.
Send one line per required pipe combination, followed by the finishing and delivery instructions. Include the engineer-approved standard and edition, grade, service requirements, diameter, wall, length, quantity, coating, inspection scope and named destination. The returned offer should pair that list with a producing location, exceptions, included costs and dated handoffs.
New LSAW capacity can provide another sourcing option if a plant is able to accept the specified work and can produce pipe within a given time frame. Keep investment announcements in a future-supplier list. A current contract is awarded based on the producing mill, route and specified delivery date.
In August 2025, the Arkansas Economic Development Commission announced that Welspun would build a $150 million LSAW mill and coating facility in Little Rock. This is different from the $100 million HFIW expansion that Welspun announced in 2024. This reference cites Welspun’s investment announcement and doesn’t state when the facility would be completed.
Standards also change while projects are being procured. The American Petroleum Institute announced the 47th edition of API Specification 5L in June 2026. Engineering should establish the required API 5L edition and applicable adopted requirements before suppliers price the work. A newer catalogue reference isn’t a reason to silently alter an existing order.
A manufacturer forms steel plate into a pipe and joins its longitudinal edges using the submerged arc welding process. Large-diameter LSAW pipes are considered for pipeline and structural orders with suitable specifications. The name describes the manufacturing route. Grade, dimensions, tests and coating identify the actual product being purchased, while the engineer-approved service requirements determine whether it fits the intended application.
Start with the required combinations of diameter, wall, grade and length, then add quantity, coating, inspection and the named destination. Reliable suppliers return their producing source and exceptions against that list. For an urgent small lot, suitable stock can be a useful starting route. For new production, the mill allocation and finishing schedule belong in the comparison alongside price and required records.
The terms describe different features, so they aren’t opposing quality grades. A longitudinal pipe can be welded internally and externally. DSAW also shouldn’t be confused with double-seam construction, where two longitudinal seams join separate plate sections. Use the seam arrangement and manufacturing method specified for the order when comparing offers, rather than treating the abbreviated label as a complete pipe description.
A plant suited to long production runs may not suit an urgent stock purchase. Compare the actual producing route, finishing scope and offered schedule.
Start with a stock inquiry for a few replacement lengths. Move to new production if the available material can’t meet the project requirements.
Send Synbase the pipe schedule, coating requirements and delivery destination. Use the LSAW welded pipe product page to begin the product discussion, and attach the same order schedule to every quotation request.
Examples of manufacturers use attributed public product information. In the case of this hypothetical price comparison, no factory interview, on-site delivered-order performance study, or current market price survey was performed.
Synbase Steel supplies steel pipe, fittings, flanges, valves and OCTG for oil and gas, petrochemical, power, water and industrial projects. Our technical guides are written to help buyers compare standards, grades, dimensions, coatings, inspection requirements and commercial terms before sending an RFQ.
We focus on practical specification work: matching pipe process to service conditions, checking wall thickness and end finish, reviewing MTC and NDT requirements, and clarifying documentation before production or shipment.
Project support across seamless pipe, ERW, LSAW, SSAW, buttweld fittings, forged flanges, valves and oilfield tubulars.
Specification review for ASTM, ASME, API, EN and DIN standards, including material grade, pressure class, coating and inspection scope.